PVD vs Electroplating vs Lacquer: Choosing a Finish for Decorative Metalwork
A brass pendant, stainless-steel chandelier and mild-steel wall light can be made to look similar in a photograph, yet behave very differently in service. The finish is not simply a colour choice. It is a surface system built around a substrate, preparation process, coating or film, and the environment in which the object will be used.
For architects, interior designers and project teams, the useful question is not “Which finish is best?” It is “Which finish system is suitable for this metal, geometry, use environment, appearance target and maintenance plan?”
1. What each process actually does
Electroplating
Electroplating uses an electric current to deposit a metal coating from an electrolyte onto a conductive component. Depending on the specified system, the deposited layer may provide colour, brightness, levelling or corrosion protection. Decorative finishes can include nickel, chromium, copper alloys and other metallic layers, often arranged as a multi-layer stack.
The final result depends heavily on surface preparation, the substrate, the sequence and thickness of layers, and the quality of rinsing and process control. A name such as “antique brass” describes an appearance, not a complete technical specification.
Physical vapour deposition (PVD)
PVD is a family of vacuum processes in which material is vaporised and deposited as a thin film. Decorative PVD can produce metallic colours and hard, wear-resistant surfaces. It is often used on stainless steel and can also be applied to other substrates when the full preparation and coating system is compatible.
PVD is not a universal protective shell. Many PVD films are very thin, and their corrosion performance depends on film structure, defects, the substrate and any underlayers. Complex shapes and recessed areas may be difficult to coat uniformly because deposition can be directional. A PVD colour on brass may therefore require suitable levelling and barrier layers beneath it.
Lacquer and clear protective coatings
Lacquer is a liquid-applied organic coating that cures or dries to form a protective film. Clear lacquer can help preserve a polished or coloured metal appearance by limiting direct contact with air, moisture and handling. Pigmented or tinted coatings can also create a chosen colour.
Performance depends on resin chemistry, film thickness, curing, surface preparation, exposure to UV and moisture, and abrasion. A clear coat may scratch, wear through at contact points or age differently from the metal beneath it. Once the film is breached, localised tarnishing or corrosion can develop.
2. Comparison at a glance
| Decision factor | Electroplating | PVD | Lacquer / clear coat |
|---|---|---|---|
| How it works | Electrochemical metal deposition | Vacuum deposition of a thin film | Liquid-applied organic film |
| Main strengths | Broad process options; good control of metallic appearance and layer stacks | Hard decorative films; many metallic colours; useful wear resistance | Can preserve a natural metal appearance; can be applied to complex shapes depending on coating process |
| Important limitations | Bath chemistry, waste treatment and process control matter; results depend on the complete layer stack | Equipment and processing cost; line-of-sight limitations; thin-film defects can expose the substrate | Can scratch, yellow, soften or wear depending on chemistry and exposure |
| Substrate considerations | Must be conductive and properly prepared; adhesion and interlayers are critical | Substrate and pre-treatment must be compatible; underlayers may be needed | Surface must be clean and compatible with the coating; edges and joints need attention |
| Maintenance question | Can the finish be repaired or replated consistently? | Can the coating be matched or renewed if damaged? | Can the coating be recoated without changing colour or sheen? |
| Best specification practice | State substrate, layer sequence where known, appearance sample and test requirements | State substrate, preparation, colour reference, coating system and performance tests | State coating type, gloss, colour, application coverage and expected maintenance |
This is a process-level comparison, not a durability ranking. A well-controlled electroplated system may outperform a poorly prepared PVD component, and a suitable lacquer may be the right choice for a low-contact decorative surface.
3. Start with the substrate, not the colour name
The same finish name can look different on polished brass, brushed stainless steel and mild steel. The substrate affects the base colour, reflectivity, surface texture, preparation method and likely failure modes.
Before choosing a finish, confirm:
- Base metal: brass, stainless steel, aluminium, mild steel or another alloy.
- Surface condition: polished, brushed, cast, machined, welded or textured.
- Geometry: deep recesses, narrow gaps, joints and internal faces can complicate coating coverage.
- Environment: dry interior, humid coastal site, bathroom, poolside or outdoor exposure.
- Contact and cleaning: frequent handling, abrasive cloths, cleaning chemicals and fingerprints affect appearance over time.
- Repair expectations: whether small damage can be touched up, whether the component can be removed, and whether a replacement can be colour-matched.
For decorative lighting, also check how the finish behaves around welded joints, drilled holes, threaded fittings and edges. These areas often reveal differences between a sample coupon and a completed fixture.
4. Colour consistency needs a reference
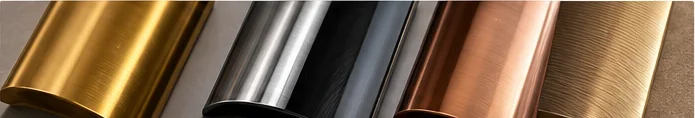
Terms such as brushed gold, champagne, antique brass, bronze and rose gold are not universal colour standards. Different processes and suppliers can produce visibly different results under the same label. Polishing direction, gloss, film thickness, substrate colour and illumination all affect perceived appearance.
For a multi-fixture project, approve a physical sample against a defined reference. Where colour is critical, record the sample ID, substrate, process, gloss or sheen, viewing conditions and acceptable variation. Instrumental colour measurement, such as CIELAB values, can support quality control, but it should complement rather than replace an agreed visual standard for reflective metallic surfaces.
Do not approve only a small flat coupon when the finished product has curved tubes, cast details, perforations or welded assemblies. Ask to inspect a representative component or first article.
5. What durability tests can and cannot tell you
A finish claim such as “scratch-proof” or “corrosion-proof” is not a useful specification. Request test evidence that reflects the actual failure risk and intended environment.
Depending on the product and exposure, relevant evaluation may include adhesion, abrasion or wear, colour change, humidity and corrosion testing. ISO 9227 describes salt-spray testing methods, but a salt-spray result alone does not predict service life in every real environment. The test method, duration, acceptance criteria, substrate and coating system must be stated. Decorative PVD research also notes that film defects and substrate preparation can materially affect corrosion performance.
A test report is meaningful only when it identifies the tested system and the acceptance criteria. A report for one substrate or colour should not automatically be treated as proof for another.
6. A practical specification checklist
For a decorative metal fixture, include the following in the finish schedule or purchase specification:
- Base metal and surface preparation.
- Finish process or complete coating system, where specified.
- Approved physical sample and colour/texture reference.
- Required faces and areas to be coated, including edges, joints and concealed visible areas.
- Intended service environment and cleaning method.
- Applicable performance tests, test conditions and acceptance criteria.
- Repair, touch-up and replacement expectations.
- Approval requirements for production samples and batch consistency.
Where a supplier uses a proprietary process, the project team may not need every bath or deposition parameter. It still needs enough information to identify the system, assess suitability and hold production to an approved standard.
Conclusion
Electroplating, PVD and lacquer solve different surface-engineering problems. Select the system by matching substrate, geometry, environment, appearance and maintenance expectations, then verify it with representative samples and relevant test evidence. A finish schedule that records only “gold” or “bronze” leaves too much room for variation.
References
- Vorobyova, M. et al. (2023). PVD for Decorative Applications: A Review. Materials, 16(14), 4919. Reviews decorative PVD processes, substrate preparation, defects and testing.
- International Organization for Standardization. ISO 9227: Corrosion tests in artificial atmospheres, salt spray tests. Check the applicable edition and product-specific requirements before specifying.
- OECD. Metal Finishing. Background on metal-finishing processes and vacuum deposition.